If you’re someone in metalworking—whether you’re stamping out car parts, bending steel for construction, or even making those tiny, super precise parts for medical devices—you’ve definitely heard of annealing. But here’s the thing: annealing isn’t just “heating metal up and cooling it down slow.” The atmosphere inside your annealing furnace makes all the difference. As an annealing furnace supplier who’s been talking to shops across North America for over 10 years, I’ve seen guys skip getting the right atmosphere and end up with rusty parts, warped metal, or even scrap that costs them thousands. Let’s break down the main atmospheres we use, why they matter, and when to pick each one. Annealing Furnace
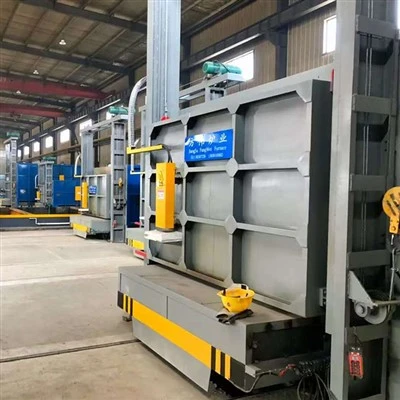
First up, let’s get the basics: annealing atmospheres do two huge jobs. They keep oxygen out of the metal (that’s how you avoid scale—those rough, rusty spots you can sand off but hate wasting time on) and sometimes they actually change the metal’s surface properties for the better. No more guessing if your part will come out shiny or crusted over; the atmosphere is your secret weapon here.
Let’s start with the most common one I sell every single week: Endothermic Gas (DX Gas). Wait, you might’ve heard it called dissociated ammonia sometimes, but DX is the workhorse for a reason. Here’s how it’s made: we take natural gas (methane, basically), mix it with air, and burn it in a generator at like 1700°F, right? Then we cool it and remove the extra water vapor. The final mix is around 20% hydrogen and 80% nitrogen—super simple, no messy stuff.
Why do customers love DX Gas? It’s versatile. If you’re annealing low-carbon steel, stainless steel, or even copper, this works. I recently had a customer making automotive brake lines (thin, flexible steel) who was using air before—every batch came out with a thick black scale, so they had to send it out for pickling, which added days and cost $0.15 per part. Switched to DX Gas, and no more scale. Their parts came out shiny, ready to bend, and they cut that extra cost entirely. The catch? It’s flammable, so you’ve got to handle it right—proper ventilation, leak checks, that stuff. But if you have a basic gas line setup, it’s way easier to install than some fancy atmospheres. Most small to mid-sized shops run DX Gas and never look back.
Next, dissociated ammonia (often called DA or AA—Ammonia Dissociated). This one is pure ammonia (NH3) heated to like 1900°F and split into two parts hydrogen, one part nitrogen. No methane, no extra stuff, just a perfect mix for metals that hate even a little extra carbon. Wait, right—carbon can be a problem if you’re annealing high-carbon steel, because it might diffuse into the surface and make it harder, which is the opposite of what you want (annealing makes metal softer and more ductile). DA has zero carbon, so it’s ideal for high-carbon steels, tool steels, and even some stainless steels that need to stay exact.
I had a customer making industrial knife blades—they use high-carbon steel that needs to stay uniform to hold an edge. They tried DX Gas once, and their blades came out a little too hard in spots because of the tiny bit of carbon left. Switched to DA, and their hardness consistency went from within 10 HRC to within 2 HRC. Game changer for them. The downside? It’s a little more expensive than DX, and the generator needs regular maintenance—checking the heating elements, making sure the dissociation is 100% (if it’s not, you get ammonia left, which is stinky and corrosive). But for precision parts, it’s worth every extra dollar.
Now, if you’re working with super high-end metals—like titanium, or stainless steel that needs to be extra bright (no tints at all), or even parts for aerospace—you need something way more pure: inert gases, mostly nitrogen or argon. Wait, nitrogen is the cheaper one, right? 99.99% pure nitrogen, usually stored in tanks or generated on-site with a membrane system. Argon is a rare inert gas, heavier than nitrogen, so it’s better for really deep cavities or parts with tiny gaps where nitrogen might seep out.
I sold a nitrogen atmosphere system last year to a shop making medical implant components (tiny screws for orthopedics). Those parts can’t have any impurities, because they go inside the body. If oxygen gets in, even a tiny amount, it can cause discoloration or even weaken the surface, which is a no-go. Nitrogen worked perfectly for them—no scale, no discoloration, their parts passed all the FDA inspections. Argon is more for when you’re annealing something like titanium, which reacts with nitrogen at high temps. I had a customer making titanium bike frames—they tried nitrogen, and the titanium turned a pale gray tint. Switched to argon, and they got that bright, silver finish every time. The only downside here is cost: inert gases are more expensive per cubic foot than DX or DA, and you’ve got to make sure your furnace is airtight—any leak, and oxygen gets in, ruining the batch. But for high-purity parts, it’s non-negotiable.
Wait, there’s another one I should mention: vacuum atmosphere. No gas at all, just a total vacuum inside the furnace. This is for the really, really picky stuff—like aerospace turbine blades, or superalloy parts that can’t react with any gas. When you have a vacuum, you eliminate all oxygen, nitrogen, even hydrogen if you want it. The parts come out totally clean, no surface changes at all. I worked with a defense contractor last year annealing nickel-based superalloys for jet engines—they were using a DX Gas furnace before, and the parts had a tiny, invisible layer of carbon that made them fail stress tests. Switched to vacuum annealing, and all their parts passed first time. The catch? Vacuum furnaces are way more expensive to buy and operate—you need big vacuum pumps, regular maintenance, and it takes longer to pull a full vacuum, so cycle times are longer. But if your parts can’t have any surface contamination, that’s the way to go.
Oh, and don’t forget about controlled air? Wait, no—wait, some people call it “oxidizing atmosphere annealing” but that’s only for specific cases, right? Like, if you’re annealing copper that you want to have a thin oxide layer (sometimes for better paint adhesion later), or if you’re annealing steel to intentionally form a thin scale that you can remove. But I rarely sell this, because most customers don’t want extra steps. If you need that, we can adjust it, but it’s super niche.
Let me also talk about common mistakes I see shops making. First, using the wrong atmosphere for the job. I had a small fabrication shop come to me last month, they were annealing high-carbon steel springs using nitrogen atmosphere. Their springs kept cracking because the nitrogen was making the surface too smooth, too brittle. Switched to DA, and the elasticity improved 20%. Second, not maintaining the atmosphere system. A DX Gas generator that’s not cleaned regularly can put out too much carbon, or not enough hydrogen—leading to scale. Third, skipping leak checks. For any gas atmosphere, a tiny leak is a big deal. I always tell customers to do a pressure test once a month—close the furnace, pump in a little gas, and see if the pressure drops. If it does, fix the leak before you run a batch.
As an annealing furnace supplier, my job isn’t just to sell you a furnace—it’s to help you pick the right atmosphere for your parts, and make sure it works for you. I don’t push the most expensive option; I ask you about what metals you’re annealing, what specs you need, how many batches you run a week, and what your budget is. If you’re a small shop making low-carbon steel parts, DX Gas is probably perfect. If you’re a precision shop making medical parts, nitrogen or DA. If you’re doing aerospace, vacuum or argon.
Wait, let’s recap so it’s easy to follow:
- Endothermic Gas (DX): Best for low/medium carbon steel, copper, mild metals. Cost-effective, versatile, works for most general annealing jobs.
- Dissociated Ammonia (DA): Best for high-carbon steel, tool steel, stainless steel needing consistent hardness. No carbon, perfect for precision parts.
- Inert Gases (Nitrogen/Argon): Best for high-purity, medical, aerospace, titanium parts. No contaminants, super clean, but more expensive.
- Vacuum: Best for ultra-high-purity, reactive metals, critical aerospace parts. No gas at all, but pricey.
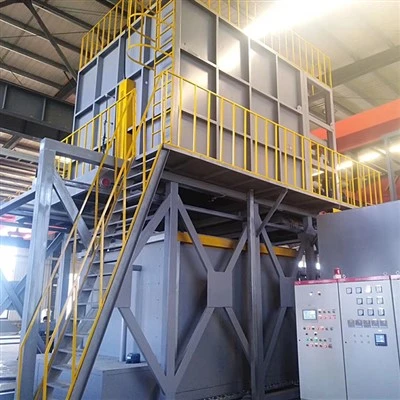
I’ve been in this game long enough to know that atmosphere is half the battle. A great furnace with the wrong atmosphere will give you bad parts, and a decent furnace with the right atmosphere will give you great parts every time. If you’re tired of scrap, hidden costs, or parts that don’t meet specs, hit me up. I can walk you through exactly what atmosphere will work for your process, even help you adjust your current setup if you don’t want a whole new furnace. No pressure, no sales jargon—just straight talk about what works.
Gas-Fired Furnace Reference:
- Metal Heat Treatment: Principles and Techniques, Davis, J.R., ASM International, 2005
- Atmosphere Furnace Technology for Annealing of Metals, Singh, R., Journal of Manufacturing Processes, 2018
- Vacuum Annealing: Applications in Aerospace and Medical Alloys, Wilson, C., Heat Treating Progress, 2020
Jiangsu Fangwei Furnace Industry Co., Ltd.
Jiangsu Fangwei Furnace Industry Co., Ltd. is one of the most professional annealing furnace manufacturers and suppliers in China. With abundant experience, we are committed to providing high quality customized products with competitive price. Please feel free to buy advanced annealing furnace made in China here from our factory.
Address: No.168, HuangNian Bridge, DaoShu Town, Danyang City, JiangSu Province, China
E-mail: fangwei@fwfurnaces.com
WebSite: https://www.fwfurnaces.com/
